


 Scan QR Code
Send My Request
Winning the 4K/8K Era: "Zero Distortion" Mold Design and Injection Molding Processes for Underwater Camera Optical Ports
2026-08-03
Underwater camera and underwater camera housing demand precision to eliminate optical distortion. Best reveals mold design and injection molding techniques that ensure zero distortion in 4K/8K optical ports, enhancing image clarity and durability for advanced underwater imaging.
- Why Does Your Underwater Camera Footage Always Have Glare and Distortion?
- 1. Fatal Internal Stress and the "Birefringence" Phenomenon
- 2. Optical Flow Marks Caused by Gate Design Errors
- 3. Microscopic Imperfections on the Mold Surface
- BEST's Optical-Grade Solution: Challenging the Ultimate Precision Injection Molding Process
- Core Strategy 1: Optical-Grade Mold Design and Top-Tier Steel Selection
- Core Strategy 2: Class 100,000 Cleanroom and RHCM (Rapid Heat Cycle Molding)
- Technical Benchmarking: Ordinary Injection vs. BEST Optical-Grade Precision Injection
- Case Sharing: Saving the "Vision" of an 8K Professional Underwater Video Camera
- Don't Let Your Marine Vision Be Blurred by Manufacturing Flaws
When evaluating a high-end Underwater camera, consumers and professional divers have only two intuitive criteria: first, it must not leak; second, it must shoot clearly.
In our previous articles, we delved into how to guarantee "no leaks" through structural waterproofing and material weather resistance. Today, the engineering team at Guangzhou Best Plastic Products Co., Ltd. (BEST) will shift the focus to the "eyes" of the underwater camera—the transparent Dome Port or Flat Port.
As camera sensor resolutions soar to 4K and even 8K, any minute optical flaw is mercilessly magnified. A transparent plastic window costing just a few dollars, if possessing injection molding defects, is enough to ruin a top-tier lens group worth thousands. In the manufacturing of optical-grade transparent components, the margin for error in mold design and precision injection molding approaches absolute zero.
Why Does Your Underwater Camera Footage Always Have Glare and Distortion?
When designing transparent ports, many R&D teams often only consider the light transmittance of the material (such as choosing high-transmission PC or PMMA) but ignore the "optical traps" inherent in the physical molding process of polymers. If your underwater camera experiences edge distortion, astigmatism, or bizarre glare during testing, the culprits are usually the following three major manufacturing defects:
1. Fatal Internal Stress and the "Birefringence" Phenomenon
During the injection molding of high-transparency plastics (like Polycarbonate PC), if the mold temperature is uneven or the injection pressure is too high, polymer chains are forcibly stretched and frozen inside the product, creating massive internal stress. This internal stress not only makes the product highly susceptible to cracking under deep-sea high pressure but also triggers the optical phenomenon of "birefringence." When light passes through a lens port containing internal stress, the light path is distorted, directly causing ghosts, color separation, or edge blurring in the camera's footage.
2. Optical Flow Marks Caused by Gate Design Errors
Molten plastic is injected into the mold cavity through a gate. If the location or size of the gate is improperly designed, the plastic will produce wavy flow marks as it flows within the cavity. Even if these flow lines are so subtle they are nearly invisible to the naked eye, under the focus of an 8K lens or the illumination of intense underwater fill lights, they turn into severe interference stripes, completely ruining the purity of the image.
3. Microscopic Imperfections on the Mold Surface
The surface finish requirement for an underwater camera lens port reaches rigorous optical grades (such as SPI A1 or higher). If the mold steel contains impurities, or the polishing process leaves microscopic polishing lines, a diffuse reflection layer will form on the surface of the injected transparent part. This not only reduces light transmittance but also makes the overall image look "soft" and lack sharpness.
BEST's Optical-Grade Solution: Challenging the Ultimate Precision Injection Molding Process
Manufacturing a high-standard optical port for an Underwater camera is a top-tier battle integrating material science, fluid dynamics, and micro/nano machining. Relying on our profound accumulation in the field of high-end optical injection molding, BEST has summarized a hardcore solution from blueprint to mass production:
Core Strategy 1: Optical-Grade Mold Design and Top-Tier Steel Selection
-
Interference-Free Gate Design: During mold design, BEST engineers use high-precision mold flow analysis software to ingeniously hide the gate location in non-optical visual areas (such as within the edge assembly groove). We typically use fan gates or film gates to ensure the molten plastic advances smoothly with a uniform melt front, completely eliminating flow marks and jetting.
-
Top-Tier Mold Steel and Nano-Level Polishing: We absolutely do not use ordinary S136 steel. For high-end lens ports, we use pure optical-grade mold steel treated with Electro-Slag Remelting (ESR) (such as Swedish Assab Stavax ESR). This steel has no microscopic pores internally. Combined with the pure hand-grinding and optical polishing of BEST's senior craftsmen, we ensure the mold cavity is as flawless as a mirror.
Core Strategy 2: Class 100,000 Cleanroom and RHCM (Rapid Heat Cycle Molding)
-
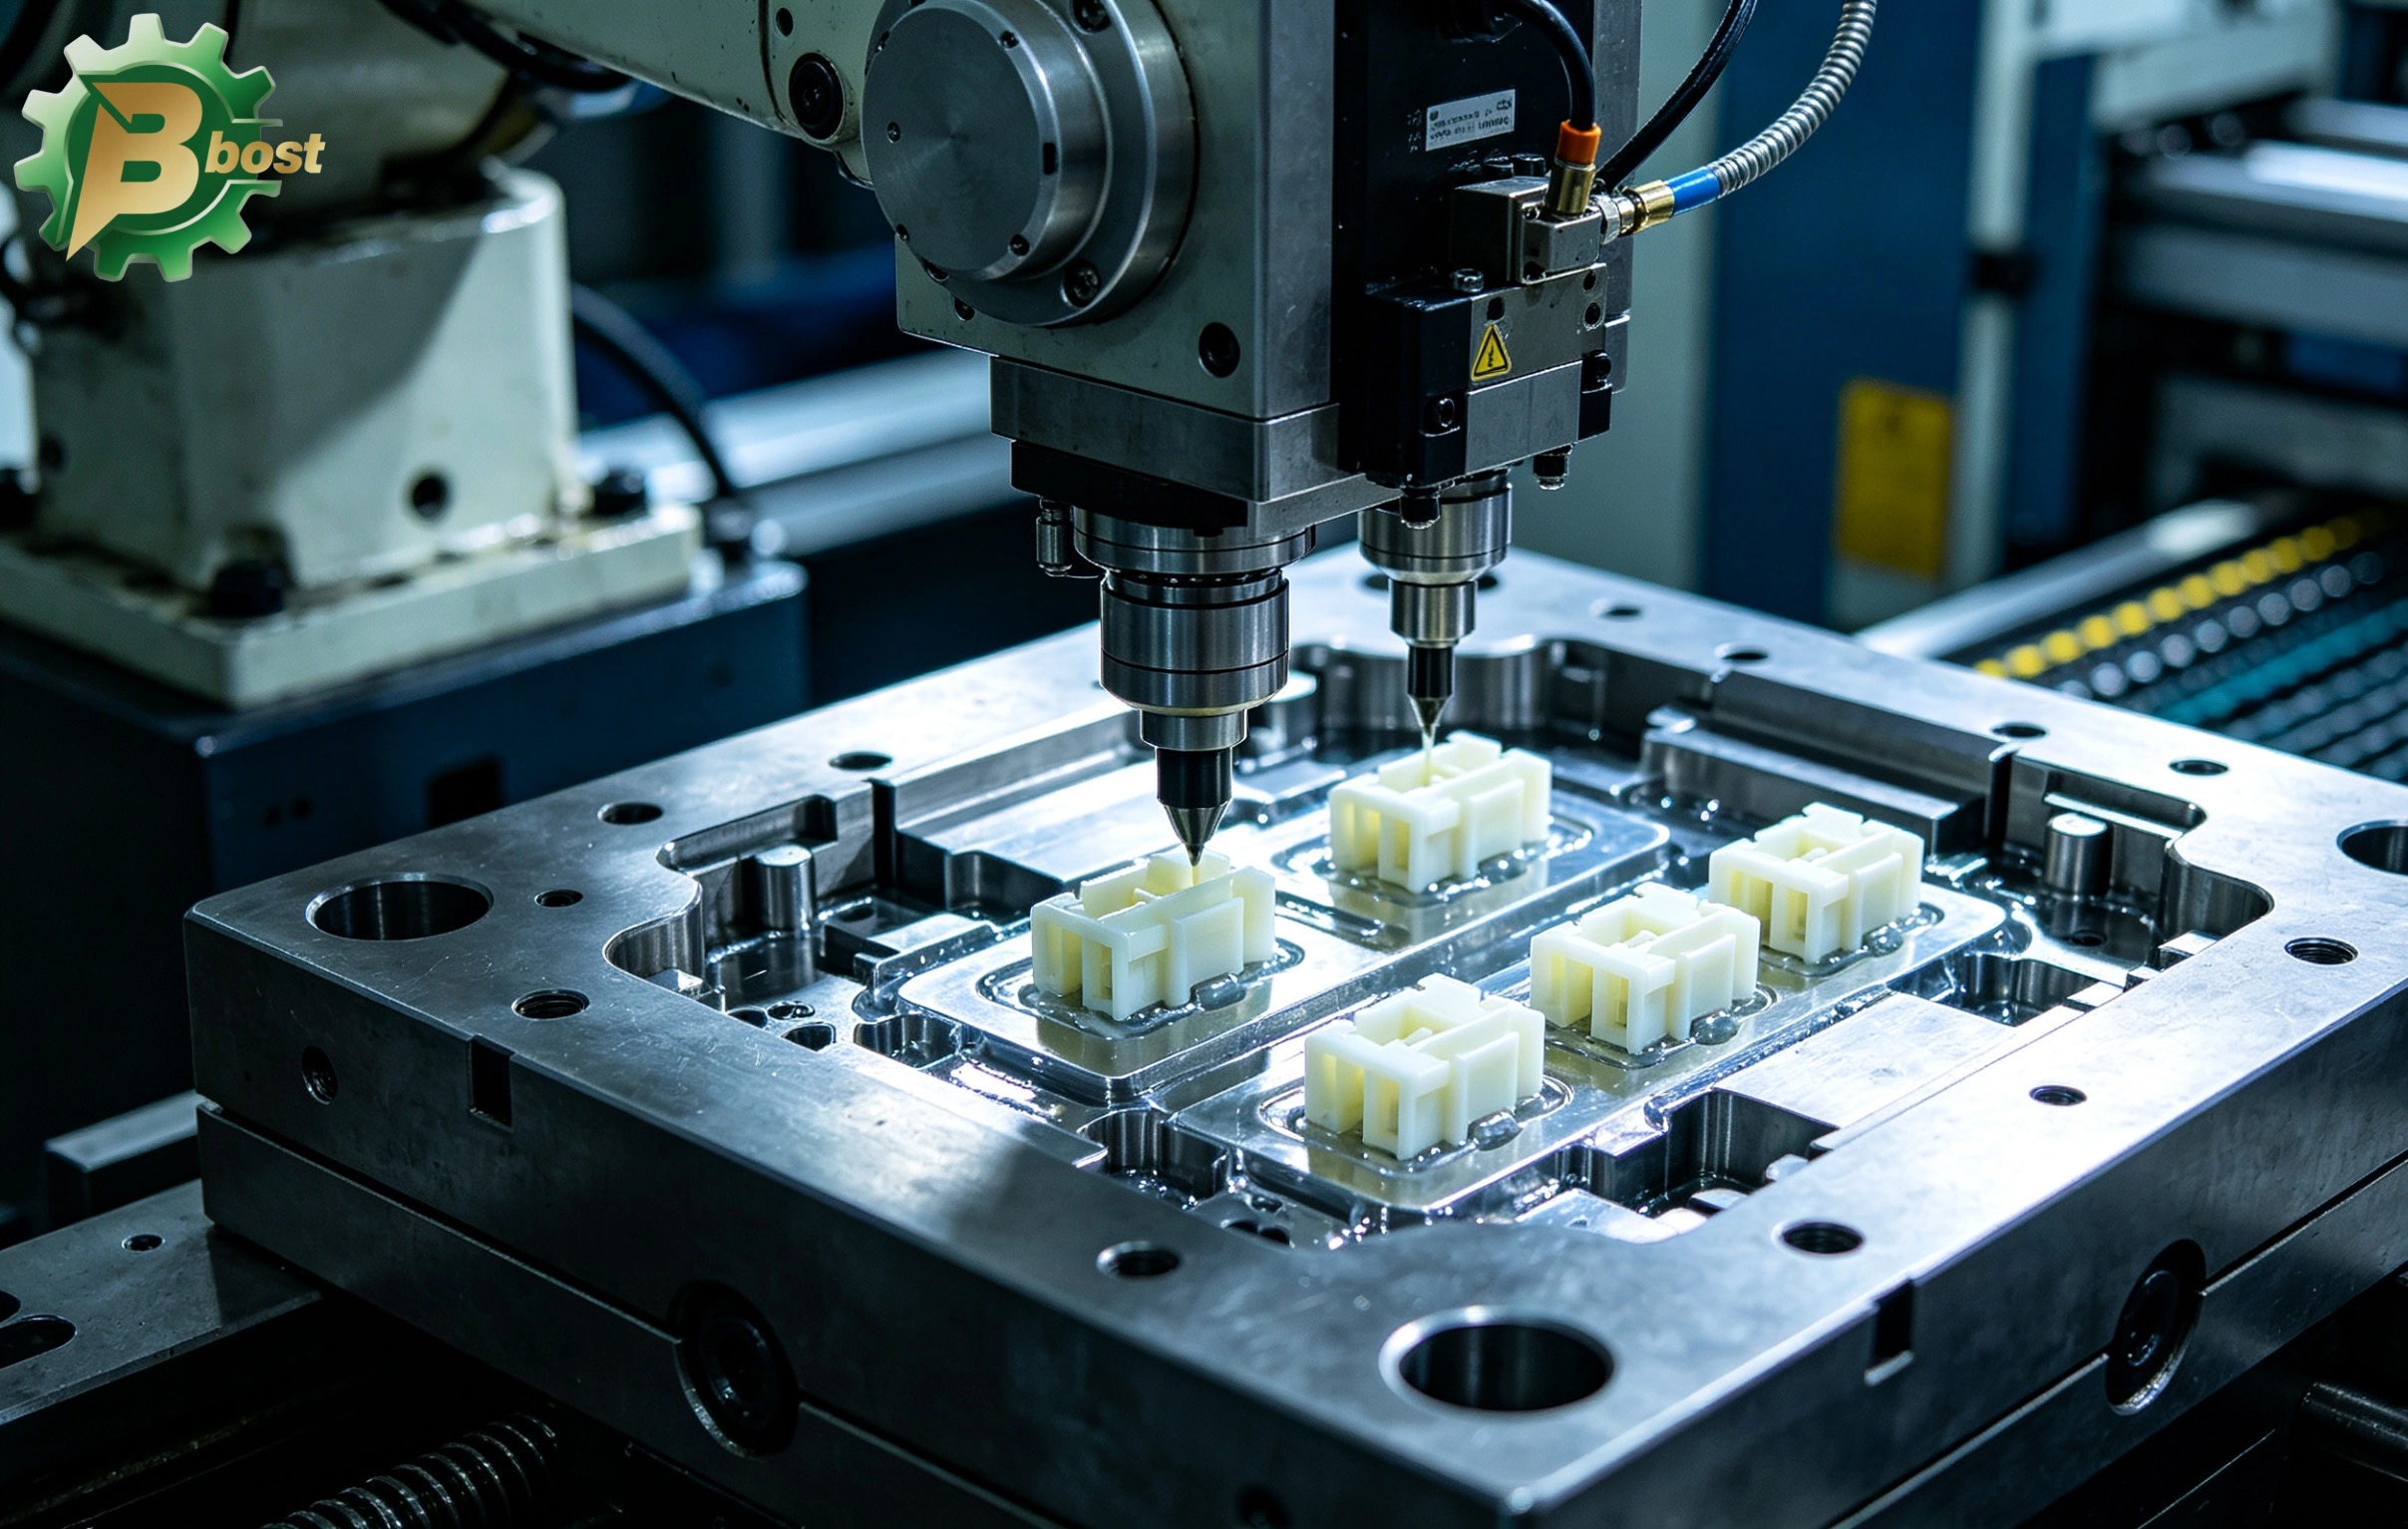
Eliminating Impurities and Black Spots: Optical transparent parts are most vulnerable to airborne dust. We conduct the precision injection molding of transparent parts in a Class 100,000 dust-free cleanroom. From automatic dehumidifying and drying of raw materials and closed material feeding, to automatic robotic part removal, environmental pollution is isolated throughout the entire process, reducing the impurity black spot rate to the lowest in the industry.
-
RHCM Technology to Eliminate Internal Stress: To completely eliminate "birefringence" and internal stress—which plague the industry—we have introduced Rapid Heat Cycle Molding (RHCM) technology. The mold temperature is instantaneously raised above the glass transition temperature of the plastic at the moment of injection, allowing the material to fill the cavity in a stress-free state, and then rapidly cooled and set. Complemented by constant-temperature annealing treatment after molding, this ensures the lens maintains perfect optical stability even under deep-sea high pressure.
Technical Benchmarking: Ordinary Injection vs. BEST Optical-Grade Precision Injection
| Evaluation Dimension | Ordinary Foundry Injection Process | BEST Optical-Grade Precision Injection | Direct Impact on Underwater Camera |
|---|---|---|---|
| Production Environment | Ordinary open workshop | Class 100k constant temp/humidity cleanroom, robotic operation | Purity: Eliminates black spots and impurities caused by dust; ensures footage has no dead pixels. |
| Mold Temp Control | Traditional water cooling, uneven and hard to control | RHCM rapid heat/cool control system, 3D conformal cooling | Optical Performance: Eliminates internal stress and birefringence; no edge distortion or astigmatism. |
| Mold Surface Treatment | Conventional mechanical polishing, invisible polish lines exist | Pure optical mold steel + manual nano-level mirror polishing | Clarity: Max light transmittance; perfectly matches 4K/8K HD image sensors. |
| Post-Molding Treatment | Directly packaged after cooling | Dedicated optical constant-temperature annealing bath | Compressive Strength: Releases residual stress, vastly reducing the risk of lens shattering in deep-sea environments. |
Case Sharing: Saving the "Vision" of an 8K Professional Underwater Video Camera
Last year, a North American client specializing in custom diving photography equipment for National Geographic and BBC documentaries encountered a thorny optical problem. Their newly developed 8K-class Underwater camera utilized a large-sized PC hemispherical Dome Port. However, during real-world testing at a depth of 100 meters, divers found that slight color separation always appeared at the edges of the image, and when shooting directly against the sun, the glare was extremely severe.
The client sent the drawings and defective samples to BEST for help. Through polarized light polariscope testing, we discovered that the original dome port had massive internal stress concentration areas near the gate and the transitional edges of the spherical surface.
BEST's Optimization and Reconstruction Plan:
-
Mold Flow Optimization: We redesigned the mold design for this dome, changing the gate from the original pin-point gate to a 360-degree ring gate, ensuring the material filled absolutely uniformly from the periphery to the center.
-
Wall Thickness Fine-Tuning: Based on the optical refractive index, we advised the client to make a 0.15mm gradient curved fine-tuning to the dome's wall thickness, making it not just a waterproof cover in the water, but acting as an optical lens correcting the underwater refractive index.
-
Cleanroom Precision Production: We moved the project into our cleanroom, utilizing all-electric injection molding machines paired with a high mold temperature and slow injection process, followed by a 24-hour precision annealing post-demolding.
After two weeks of mold modification and sampling, the new generation optical dome delivered by BEST performed stunningly in underwater field tests: the edge distortion rate dropped by 90%, and the birefringence phenomenon was completely eliminated. This underwater camera was ultimately successfully selected into that year's equipment pool for top-tier marine documentary filming.
Don't Let Your Marine Vision Be Blurred by Manufacturing Flaws
In the extreme world of high-definition underwater vision, the most expensive cost is not the purchase price of a top-tier sensor, but rather a slight flaw in a plastic lens port ruining a breathtaking moment a diver risked their life to capture. Manufacturing the optical window of an Underwater camera is the ultimate test of a factory's technical heritage.
Guangzhou Best Plastic Products Co., Ltd. (BEST) profoundly understands the dual challenges of underwater optics and deep-sea physics. We possess industry-leading cleanroom injection facilities, a top-tier mold design team, and a paranoid pursuit of optical-grade quality. We not only build robust waterproof armors for you but are committed to polishing the "deep-sea eyes" of your equipment.
Perfect image quality stems from micron-level manufacturing obsession.
👉 Visit our official website now at https://www.gz-best.com to submit your optical transparent part drawings or waterproof structural designs. BEST's engineering experts will provide you with a free optical mold flow analysis and DFM evaluation, tailoring the most cost-effective HD mass production plan for you. Let your underwater camera capture the ultimate clarity in the deep sea!
Recommended for you
The Peak Art of Custom Manufacturing According to Drawings: Comprehensive Guide to Precision Solutions for Custom Parts According to Drawing
Ending Mechanical Wear and Resonance: The Comprehensive Guide to Precision Customization and Mass Production of a Custom Rubber Pad
The Ultimate Armor for Smart Hardware: Advanced Customization and Precision Injection Molding Guide for a Custom Plastic Box
The Ultimate Weapon to Tame Vibration and Noise: Deep Dive into the Custom Process and Mass Production Logic of a Custom Rubber Bushing
Product Categories
FAQ
FAQs
What is the delivery lead time? Do you offer global logistics?
Standard products: 5–15 working days; custom modifications: 2–4 weeks. We support global air/sea freight and provide export customs clearance documents (including REACH/UL certifications).
Can Best customize modified plastics with special properties?
Yes! We offer modification services such as reinforcement, flame retardancy, conductivity, wear resistance, and UV resistance, for example:
• Adding carbon fiber to enhance stiffness
• Reducing the coefficient of friction through PTFE modification
• Customizing food-grade or medical-grade certified materials
What is the minimum order quantity (MOQ)? Do you support small-batch trial production?
The MOQ for standard products is ≥100kg. We support small-batch trial production (as low as 20kg) and provide mold testing reports and performance data feedback.
How do I select the appropriate engineering plastic grade for my product?
Selection should be based on parameters such as load conditions (e.g., pressure/friction), temperature range, medium contact (e.g., oil/acid), and regulatory requirements (e.g., FDA/RoHS). Our engineers can provide free material selection consulting and sample testing.
What are the core advantages of Best engineering plastics compared to ordinary plastics?
Best engineering plastics feature ultra-high mechanical strength, high-temperature resistance (-50°C to 300°C), chemical corrosion resistance, and wear resistance. Compared to ordinary plastics, their service life is extended by 3 to 8 times, making them suitable for replacing metals in harsh environments.
You may also like
Custom Plastic Knobs Precision Injection Molded
More Details →
Custom Plastic Knobs Precision Injection Molded
Custom Injection Molded Parts from Drawings
More Details →
Custom Injection Molded Parts from Drawings
Underwater Camera Shell Custom Plastic Molding
More Details →
Underwater Camera Shell Custom Plastic Molding
Leave a Message
Have any questions or concerns about our products? Please leave us a message here, and our team will get back to you promptly.

24 hours quotes delivered
Submit CAD files, get quote in 24 hours

No MOQ required
From prototyping to high-volume

±0.02 mm Precision
Advanced CNC with full inspections

1,000+ tons in stock
26 materials ready to ship
© 2026 BOST. All Rights Reserved.